
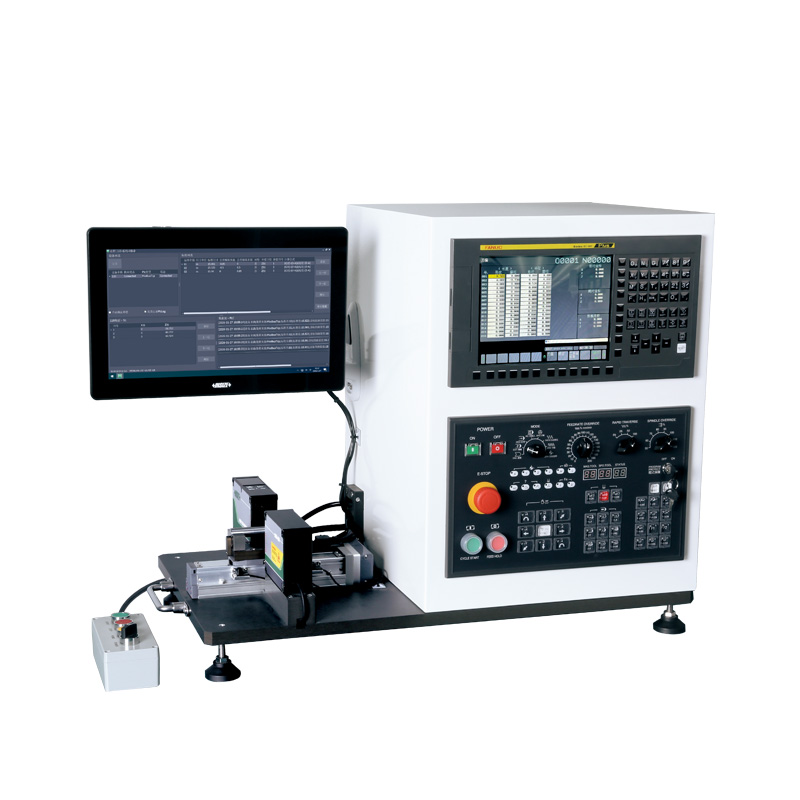
Automatic Tool Compensation System
Code: ATU-03A
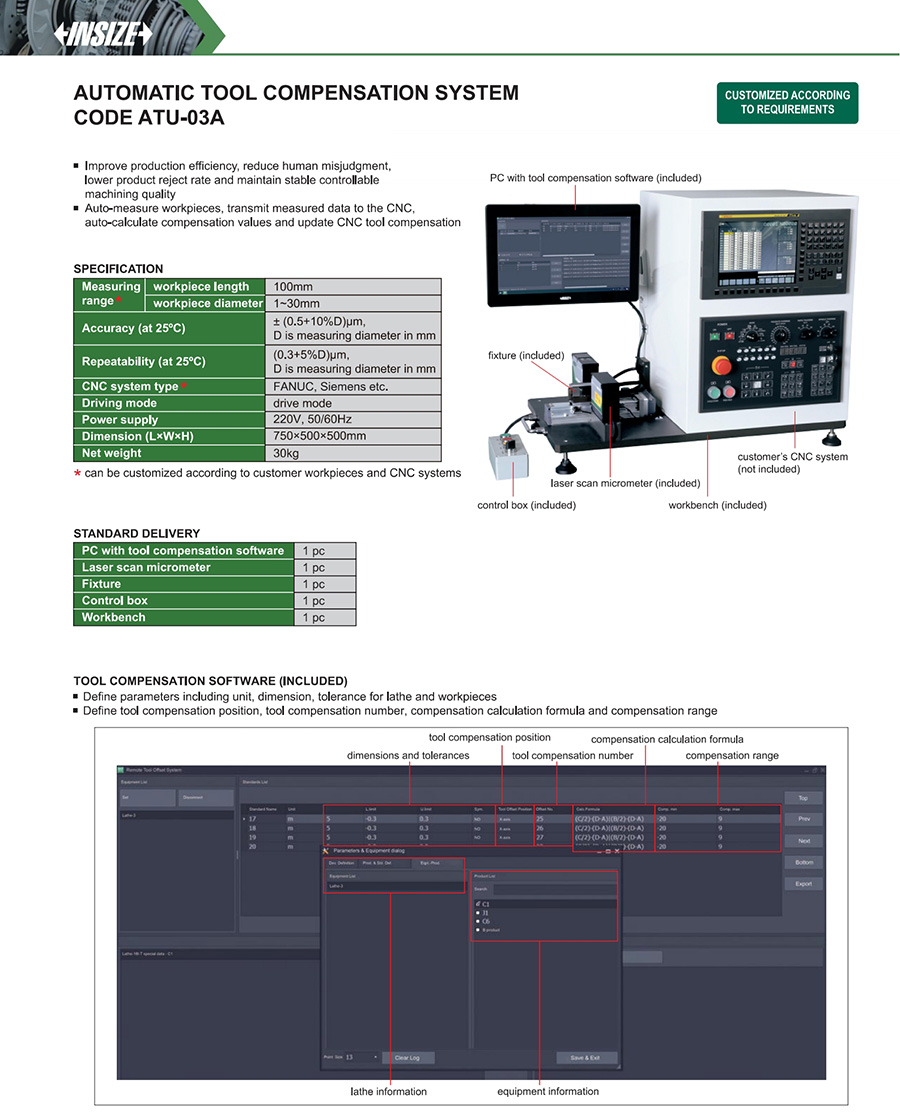
Improve production efficiency, reduce human misjudgment, lower product reject rate and maintain stable controllable machining quality
Auto-measure workpieces, transmit measured data to the CNC, auto-calculate compensation values and update CNC tool compensation
View the complete
product specifications
FAQ
What are the core functions of this system?
● The system provides three core functions:
1.Digital measurement and real-time statistical analysis of quality data;
2.Automatic tool compensation based on measurement results;
3.Real-time dynamic SPC process control.
In simple terms, it provides a closed-loop “Measure – Calculate – Compensate” process. After measurement, the system automatically analyzes the data, calculates the tool compensation value, and writes it to the CNC system without manual intervention.
How does automatic tool compensation work?
The system uses digital measuring tools to collect the actual dimensions of the workpiece and compares them with the nominal values. It then calculates the compensation value according to the preset formula and transmits the compensation value to the corresponding tool compensation address of the CNC system via Ethernet. The CNC system automatically applies the new tool compensation value during the next machining cycle, correcting machining deviations in real time.
How is the compensation value calculated? Can the formula be modified?
The compensation formula can be customized.
The system provides two default calculation methods: (C/2) – (D-A) or (B/2) – (D-A), where C is the tolerance zone width, D is the measured value, A is the nominal value, and B is the upper tolerance limit.
Customers can adjust the calculation logic in the software according to their process requirements.
Under what conditions is compensation triggered? Is there a range where no compensation is applied?
● The system uses a graded compensation logic. Taking a tolerance of 40±0.02 mm as an example:
Measurement value within 39.98–40.02 mm (within the tolerance zone) → No compensation is triggered to avoid frequent minor adjustments.
Measurement value within 39.95–39.98 mm or 40.02–40.05 mm (warning range) → The compensation value is calculated according to the formula and written to the CNC system.
Outside the warning range → The system identifies the measurement as abnormal and requires manual confirmation.
Which CNC address is the compensation value written to?
The compensation value is written to the CNC tool compensation address. The specific address can be configured and assigned in the software according to the CNC system configuration and process requirements.
Which CNC systems are supported?
The system supports mainstream CNC systems. This equipment is custom-made. Compatibility shall be confirmed upon provision of the CNC model.